3D Car Floor Mats Factory: Precision Production Behind Custom Interior Protection
2026-09-10
You rarely think about the mat under your shoes until it slides, curls, or soaks through. That's exactly why 3D car floor mats have evolved from a simple accessory into essential interior armor—and why their production demands far more than a one-size-fits-all stamp. At FANDEWEI's factory, every mat begins as a digital map of the vehicle's footwell, then moves through precision cutting, heat-molding, and edge-sealing to mirror each curve and dead pedal. The goal isn't just a piece of rubber; it's a custom-fit shield for your cabin. But how does a raw polymer sheet transform into that satisfying, glove-like fit? Step inside the process that treats floor protection as seriously as the dashboard above it.
Inside the Factory: How Digital Scanning Shapes Every Mat
On the line, a scanning rig passes over every mat before trimming. It's not snapping photos for a catalog; it's reading the surface at sub-millimeter resolution, checking rebound, pile height, and edge straightness. If a batch of rubber cures a bit too soft or the weave pulls slightly off-axis, the scanner flags it before the mat reaches the cutting die.
That scan becomes a point cloud compared against the approved CAD file. The system doesn't just look for obvious defects; it catches subtle drift like a logo that's rotated half a degree or a beveled edge that's lost its crispness. Operators see a heat map of variance and can recalibrate the extruder or loom without stopping the entire shift.
Digital scanning also closes the loop between the factory floor and the design studio. Instead of waiting for customer complaints or quarterly audits, engineers pull scan trends and adjust tooling or material suppliers. The result is less scrap, fewer reworks, and mats that feel identical from the first unit to the ten-thousandth.
Not Just Trimmed to Fit: The 3D Difference in Layering
Most people think of a haircut as a flat outline that simply follows the head, but 3D layering works from the inside out. Instead of just shortening the ends to a desired length, the stylist carves out weight and builds internal movement that respects the skull’s curves. Each section is lifted at a deliberate angle, so the hair falls with a natural bounce rather than lying stiff against the neck. This approach turns a basic trim into a sculpted shape that shifts and breathes as you move.
The real difference shows up in how light travels across the hair. Flat, one-length cuts reflect illumination in a single plane, but 3D layering creates pockets and ridges that catch highlights at different depths. A trained eye will pull strands upward and forward, cutting not just to remove bulk but to redistribute density where it supports the overall silhouette. The result is a cut that looks effortless on day one and even better after a few washes, because the structure was built into the hair rather than styled on top of it.
For anyone tired of haircuts that fall flat by midweek, this method changes the game. You don’t need a handful of product to recreate salon volume; the layers already hold their place and encourage natural texture. Blow-drying becomes quicker, air-drying looks intentional, and the shape grows out without losing its architecture. It’s the difference between a haircut that simply removes length and one that actually designs how your hair lives around your face.
Material Choices That Survive Mud, Snow, and Spilled Coffee
Entryways and family rooms see the worst of winter. Instead of fighting every stain, pick materials with tight, non-porous surfaces. Glazed ceramic tile and sealed concrete shrug off mud and snow, but they can feel cold underfoot. For a softer landing, look for polypropylene or olefin-blend area rugs; they hold almost no moisture, so wet dirt stays on the surface and wipes away before it turns into a stain.
Coffee spills are a different test. Natural stone and untreated cotton or linen pull liquid in quickly, leaving rings that are hard to remove. Treated wool or velvet with a soil-resistant finish gives you a few extra seconds to blot. Keep a dry cloth nearby and press gently instead of rubbing, because rubbing drives the coffee deeper into the weave.
If the same floor has to handle muddy boots and a morning latte, choose pieces you can clean individually. Modular carpet tiles or small washable rugs let you rinse or hang-dry just the dirty section. Patterns with dark flecks, heathered weaves, or a matte texture also hide the occasional missed spot far better than a light solid color.
From CAD Model to Mold: Where Custom Fit Is Engineered
A CAD model isn't a promise—it's a starting point. Once the design leaves the screen, it has to survive the realities of injection molding. Every wall thickness, boss, and snap-fit gets scrutinized for how resin will flow and cool. Custom fit starts here: with draft angles that won't scar the part, radii that reduce stress, and shutoffs that keep edges clean. Miss one detail and the 'custom' element becomes a post-molding fix.
The handoff between CAD and mold maker is rarely one-directional. It's a loop. A change to the model's undercut forces a change in the slide. A tighter tolerance on a mating surface means re-cutting the cavity. These back-and-forth passes aren't inefficiency; they're where fit gets engineered. By the time the mold is cut, the part's fit has already been tested in silicone, steel, and code.
That's the difference between a generic enclosure and a device that sits against skin or snaps into a bracket. The mold doesn't just replicate the CAD—it interprets it, compensates for shrinkage, and resolves the stacking tolerances. When someone calls it a custom fit, what they're really holding is a series of decisions made in the tooling phase. Not an afterthought. Not a lucky break. An engineered outcome.
Edge Binding and Heel Pads: Small Details, Heavy Daily Wear
Most people only notice edge binding when it starts to roll or pinch. A well-made pair uses a thin, flat seam along the toe and outer edges that sits almost invisibly against the skin. That keeps the sock from twisting around your foot during long walks, and it stops the kind of rubbing that turns into sore spots by the end of the day.
The heel pad does a quieter job but takes far more abuse. Every step drives your heel down into the shoe, and without a denser knit there, the fabric thins out fast. A proper heel pad spreads that pressure, adds a bit of cushion, and stays springy even after weeks of washing. It's not flashy, but it's why some socks still feel new after three months while others feel paper-thin.
Together, these two small parts decide whether a pair holds up to real life. They won't show up in a photo the way a bold pattern does, but after a few wears your feet will know the difference.
Why Our Production Line Rejects Mats Most Brands Would Ship
Most brands look at a finished mat and ask one question: can we sell it? Our production line asks a completely different question: would we put this in our own facility and stand on it for ten hours a day? That single shift in perspective means we reject mats that others happily box up—because we see the hairline seam misalignment, the 2mm variance in edge beveling, or the subtle rubber odor that only appears after a heat cycle. These aren't defects you notice in a product photo, but they're exactly what breaks down after six months of forklift traffic.
We also run a destructive test on every batch, not just a sample. If a mat survives 3,000 fatigue cycles but shows micro-cracking at the drainage holes, the entire run is scrapped—even if those cracks are invisible without magnification. Most suppliers would call that overkill; we call it the difference between a mat that lasts two years and one that lasts ten. The rejected mats don't go to a discount outlet either. They get ground down and recycled into our lower-tier utility line, where the performance bar is deliberately lower and clearly labeled.
The real reason for this strictness isn't noble—it's practical. A single mat failure under a CNC machine costs more in downtime than a hundred mats in lost margin. So our line is designed to reject generously, and our engineers have veto power over the sales team. That's rare, but so is a mat that never curls, never slides, and never needs replacing before the machine it sits under.
FAQ
Most factories layer several materials for structure and comfort. A common stack-up includes a wear-resistant PVC or TPE top skin, a cross-linked polyethylene foam middle for cushioning, and a brushed anti-skid backing so the mat stays put on carpet or bare metal.
Instead of relying on universal templates, technicians take laser scans of the actual floorpan or import OEM CAD data. That point cloud gets cleaned up into a digital model, which drives CNC machining of the mold so every rib and curve lines up with the car's footwell.
It starts with sheet cutting and preheating, then the layered material goes into a heated mold for compression forming. After cooling, edges are trimmed by hand or with a robotic knife, heel pads or logos are attached, and the mat passes through inspection before packing.
Because the raised sidewalls follow the floorpan's shape, spills and dirt get trapped in the tray instead of running off the edges. The rigid molded structure also stops the mat from bunching up under the pedals, which is a real safety benefit.
Workers use go/no-go fixtures to check dimensional accuracy on a set sample cadence, run abrasion and peel tests on material batches, and do a quick odor check after molding. Any batch with more than a minor edge burr is pulled for rework before it leaves the line.
Yes, if the vehicle isn't in the existing mold library, we can work from a customer-provided scan or arrange a local 3D scan. Tooling costs are higher for one-off jobs, but the process is the same as for high-volume models.
You can choose surface texture, color matching to the interior, contrasting stitching, a reinforced heel area, different backing types for carpet vs vinyl floors, and even embossed logos or model names.
From receiving the scan data to first article approval usually takes two to four weeks. The bulk of that time is mold machining and fine-tuning the trim lines; after tooling is signed off, scaling up to full production is much faster.
Conclusion
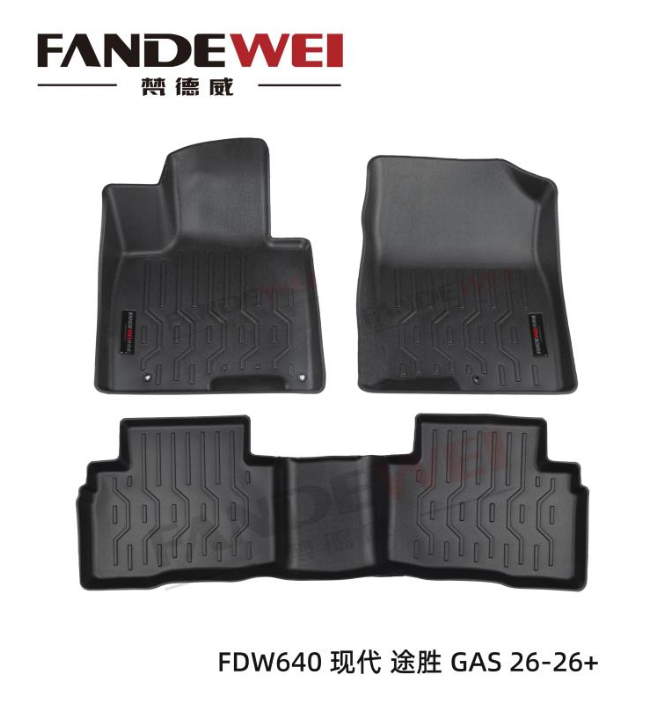
Every mat begins with a digital scan of the vehicle's footwell, capturing the exact contours, anchor points, and even the subtle rise around the pedals. That data becomes a CAD model, where each layer is engineered for a true 3D wrap rather than a flat piece of rubber trimmed to approximate size. The difference shows in the deep side walls that cradle boots and shoes, keeping slush, gravel, and melted snow from sliding onto the carpet underneath. Material selection is unforgiving: only compounds that resist cracking in subzero cold, shrugging off mud, road salt, and spilled coffee without staining or absorbing odor make the cut. Small details carry heavy responsibility—edge binding is welded, not glued, to prevent peeling under daily heel pivots, while reinforced heel pads are positioned where drivers actually plant their foot, not where a generic mold decides it should go.
From CAD to machined mold, the fit is not guessed; it is engineered tolerance by tolerance. Our production line rejects mats most brands would happily box and ship: warped edges, uneven layer lamination, slight shrinkage after cooling, or a heel pad off by a few millimeters. That rejection rate costs time and material, but it is the only way a mat earns the promise of custom interior protection. The result is a floor liner that locks into the factory retention clips, follows the transmission tunnel and door sill contours, and stays put through years of boots, road trips, and winter sludge. It is not just a mat—it is a precision-formed shield for the cabin, built from scan data, layered materials, and a refusal to let small flaws become big problems underfoot.
Contact Us
Contact Person: Jet
Email: [email protected]
Tel/WhatsApp: 8619903745266
Website: https://www.fandewei.com/